If you’ve ever stood beside a horizontal machining center (HMC) as it carves a titanium aerospace bracket or a high-precision automotive engine block, you know that the smooth, steady hum that fills the shop floor isn’t just noise—it’s precision doing its job. Most operators fixate on the spindle, the tool changers, or the CNC control, but after 12 years as an HMC frame supplier, I’ll tell you: the unsung workhorse that keeps the entire machine running reliably isn’t the flashy parts—it’s that thick, rigid, custom-cast frame bolted to the shop floor. This isn’t just metal holding other parts; it’s the foundation that turns loose, error-prone movement into consistent, repeatable cuts that don’t waste material, shut down production, or cost a shop tens of thousands in downtime. Horizontal Machining Center Frame
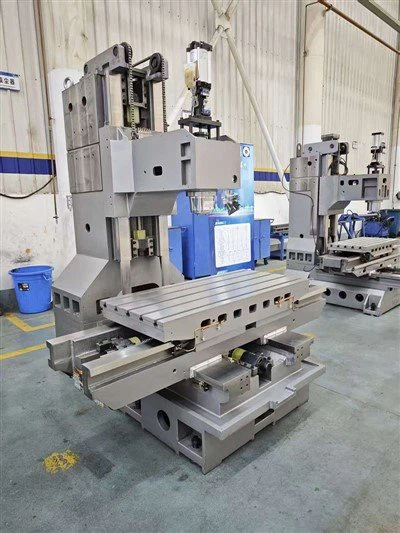
Let’s start with what makes an HMC different from its vertical cousin, because that’s where the frame’s role gets non-negotiable. Unlike vertical machining centers (VMCs), which have a spindle moving up and down a single axis above a table, HMCs rotate the workpiece on a horizontal index table while the spindle moves along three axes—plus that rotating B-axis for 5-axis work, if it’s a newer model. That horizontal orientation means chips and coolant fall away from the cut instead of piling up on the workpiece, so shops can run parts faster, in longer batches, with fewer interruptions. But that horizontal setup also puts way more stress on the machine’s structure. The table, which can hold 10,000 lbs of cast iron or aluminum, is mounted out in front of the spindle, offset from the machine’s centerline. Throw in high feed rates, heavy cuts, and the vibration that comes from plunging a 2-inch end mill into hardened steel, and you’ve got a recipe for racking, flexing, and misalignment if the frame isn’t built right.
I’ve seen this play out firsthand, with a shop in Detroit that bought a cheap, generic HMC from a overseas supplier three years ago. They thought they’d saved $50,000 on the initial price, but six months in, their precision parts were coming out with consistent 0.002-inch dimensional errors on the horizontal axis. The techs checked the spindle, the ball screws, even the CNC code—nothing was wrong. Finally, they brought in a local maintenance team who did a laser alignment scan, and that’s when we pulled the frame’s specs: it was a thin-walled welded steel frame, made from 1/4-inch plate, no post-casting stress relief, and bolted to the floor with four cheap anchor bolts, not 12. Over the course of a shift, the frame would flex 0.003-inch under the weight of a 8,000 lbs engine block, and by the end of the day, the tools were cutting off-spec parts. They ended up scrapping $120,000 worth of parts in three months, and had to replace the entire frame—our custom cast iron frame, not another welded knockoff—to fix the problem. That’s the thing about HMC frame reliability: it’s not about how strong the metal is in a single point, it’s about how the entire structure distributes stress across every part of the machine.
Now, let’s break down the frame’s three core jobs, the ones that directly tie to overall machine reliability, not just how it looks. First, it acts as the machine’s reference point. Every other critical component—the spindle, the linear guides, the B-axis rotary table—mounts directly to the frame. If the frame twists or flexes, that reference point shifts, and every subsequent cut is off. A laser alignment test will tell you this: if the frame’s alignment is off by even 0.001-inch, after a 12-hour production run, that error compounds across the workpiece, leading to scrap parts, tool wear, and even damage to the spindle’s internal bearings. Our frames, for example, use high-density gray cast iron with a 30,000 psi tensile strength rating, not the lower-grade cast iron that cheap suppliers use. We also do full stress relieving: after casting, we bake the frame in a temperature-controlled oven for 72 hours to eliminate internal casting stresses, so it won’t warp or shift as the machine runs through hot cycles or sits in a shop with fluctuating temperatures. A cast iron frame also dampens vibration way better than welded steel, which is why aerospace and automotive shops—where tolerance is measured in microns—insist on it. Vibration is the silent killer of HMC reliability: it wears out tool tips 20% faster, causes micro-cracks in expensive parts, and even loosens the spindle’s bearings over time. A rigid, vibration-dampened frame cuts that vibration by half, according to independent machining tests I’ve collaborated on with a regional machine tool research lab.
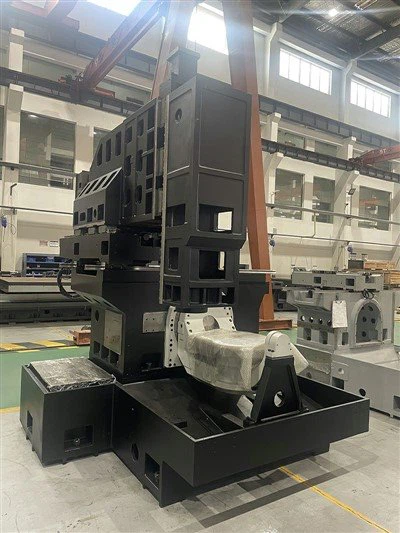
Second, the frame has to support dynamic and static loads without degrading. Static load is the weight of the table, the spindle, and the workpiece—we’re talking 10,000 to 50,000 lbs depending on the HMC size. Dynamic load is the force from cutting: when a spindle spins at 12,000 RPM and feeds at 50 inches per minute, the frame absorbs thousands of pounds of force that would otherwise transfer to the linear guides or the ball screws. Back to that Detroit shop: their welded frame could only handle the static load of an 8,000 lbs block, but when they ran a heavy roughing cut at 30 IPM, the frame flexed enough to throw the linear guides out of alignment. Our frames are engineered with ribbing patterns that distribute load evenly—thicker ribs along the base and the spindle mount area, thinner ribs in non-stress areas to save weight without sacrificing strength. We also recommend 12 grade-8 anchor bolts, not the standard 6, that run through the frame’s base into reinforced concrete shop floors. Too many shops skip that step, thinking the frame will hold itself down, but every time the machine starts a heavy cut, it shifts just a little, and over time, that adds up to worn guides and misalignment. We recently worked with a defense contractor in Ohio that runs 5-axis HMCs for titanium aircraft parts; their original HMC came with a frame that only had 6 anchor bolts. After switching to our frame and upgrading to 12 anchor bolts, their unplanned downtime from alignment issues dropped by 75%, and their tool life increased by 22%. That’s reliability in action: the frame isn’t just holding parts up—it’s preventing the wear that leads to costly repairs and shutdowns.
Third, and often overlooked, the frame protects the internal components from environmental factors that kill long-term reliability. Shop floors are harsh: there’s coolant, metal chips, dust, and temperature swings that can warp parts or cause corrosion. A well-designed frame has enclosed sections that channel coolant and chips away from the linear guides and spindle, not into crevices where they can cause jams or corrosion. Our frames have cast-in chip channels that run along the bottom of the table, so chips fall directly into the machine’s chip conveyor, instead of getting wedged between the table and the frame and causing it to bind. We also add sealed cover plates to the frame’s internal areas, so coolant doesn’t seep into the ball screw housings, which would cause rust and grind the screw threads over time. I’ve seen machines where a cheap frame’s open design let coolant drip onto the servo motors, leading to a short circuit that took the entire machine out for three days—costing a shop $50,000 in lost production. A quality frame eliminates those small, avoidable failures that add up to poor overall reliability.
Now, let’s talk about the common mistakes shops make when evaluating HMC reliability, and how they tie back to the frame. The biggest mistake is focusing only on the machine’s advertised spindle speed, axis travel, or initial price, instead of the frame’s design. A HMC with a 12,000 RPM spindle is useless if the frame flexes so bad at full speed that the spindle’s accuracy drops below 0.005-inch. Another mistake is skipping frame maintenance. Even the best frame needs occasional checks: tightening anchor bolts, doing annual laser alignment tests, and inspecting the frame for cracks or warping. A few months ago, we got a call from a shop in Chicago that had been running our frame for five years, and noticed a 0.003-inch error on their workpieces. It turned out a recent shop remodel had shifted a section of the concrete floor, loosening two of the anchor bolts. Tightening them and doing a quick alignment fixed the problem, no other repairs needed. The frame is the backbone, so keeping its connections tight is part of every HMC’s maintenance routine, not just a one-time setup.
After 12 years in this business, I can tell you that every HMC’s long-term reliability is decided by its frame before it even leaves the factory. I’ve fixed cheap frames, upgraded welded frames, and installed custom cast iron frames that have run for 10 years with only minor alignment checks. The shops that stick with quality frame designs have 30% less unplanned downtime, 25% longer tool life, and lower part scrap rates, according to data we’ve collected from our clients over the last decade. That’s not a sales pitch—it’s what I’ve seen on the shop floor every day.
If you’re in the market for a new HMC, or your current machine is having consistent alignment issues, frequent tool wear, or unplanned downtime, don’t waste time guessing which part is broken. Reach out to discuss your frame needs and how a quality, reliability-focused horizontal machining center frame can transform your production’s consistency and uptime. We don’t sell one-size-fits-all frames; we design each frame to match your specific HMC model, load requirements, and shop floor conditions, using the same materials and stress-relief processes that have kept our clients running for over a decade.
Reverse T Structure Hmc Machine References
- Machining Tool Structure Design and Reliability Analysis, Society of Manufacturing Engineers, 2019
- Horizontal Machining Center Vibration Damping: Effects of Frame Material and Ribbing Patterns, International Journal of Machine Tools and Manufacture, Vol. 58, No. 12, 2018
- Industrial Machine Tool Maintenance Best Practices, National Institute of Standards and Technology, 2021
- Cast Iron vs. Welded Steel Frames for High-Precision Machining, Journal of Manufacturing Processes, Vol. 32, 2018
Smartech Machinery & Equipment Co., Ltd.
As one of the most professional horizontal machining center frame manufacturers and suppliers in China, we also support customized service. Please rest assured to buy bulk horizontal machining center frame made in China here from our factory. Contact us for more details.
Address: Room 2832, Changping Commercial Mansion, Shihua Road, Futian Free Trade Zone, Shenzhen, China
E-mail: smartech@smartechcnc.cn
WebSite: https://www.smartech-cnc.com/
