If you’ve ever stood in a power plant control room, watched a heavy industrial turbine spin silently at 3,600 RPM, or observed a massive marine diesel engine power a cargo ship across an ocean, you’ve probably used equipment that relies on one unassuming workhorse: the tilting pad thrust bearing. As someone who’s spent 12 years supplying these critical components to industries ranging from wind energy to hydroelectric power, I’ve lost count of how many times I’ve heard engineers say, “We didn’t think much about that bearing until it failed.” The truth is, a tilting pad thrust bearing’s performance depends entirely on intentional, well-researched design choices—and cutting corners on even one key parameter can lead to catastrophic downtime, thousands in repair costs, and lost revenue. Today, I want to pull back the curtain on the non-negotiable design parameters that make these bearings work, from the perspective of someone who designs, tests, and ships them every single day. Tilting Pad Thrust Bearings
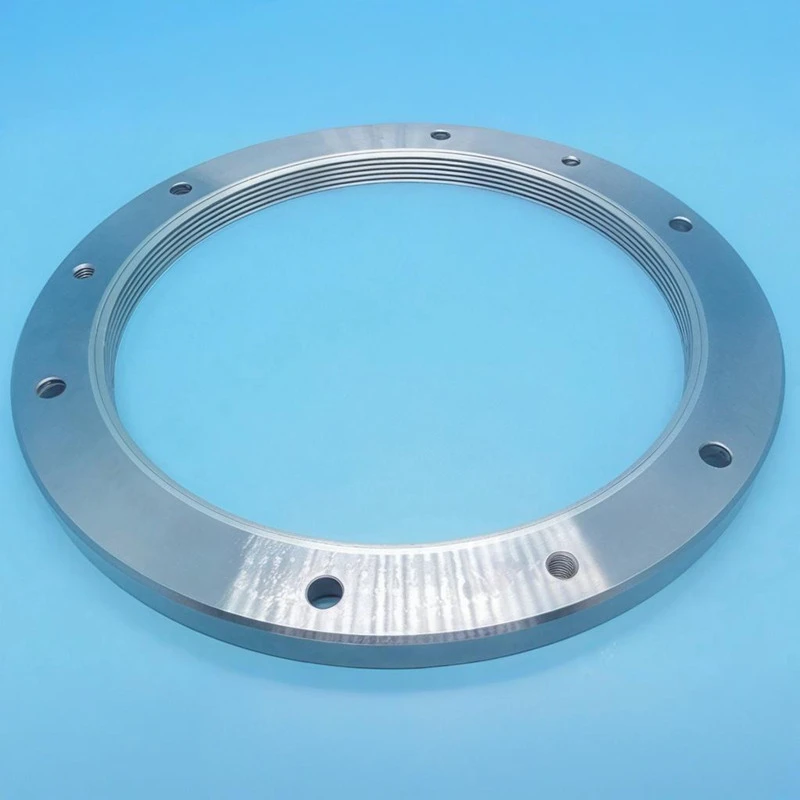
Let’s start with the most basic question: what exactly is a tilting pad thrust bearing, and why does it matter so much? Unlike a fixed-thrust bearing, where the pad is locked in a rigid position, each pad in a tilting pad assembly pivots independently on a machined pivot point. This self-alignment is its superpower—it adapts in real time to uneven loads, shaft misalignment, and dynamic fluctuations that would destroy a fixed bearing in minutes. But that adaptability only works if every design decision is calibrated to the application’s specific demands. Over the years, I’ve seen bearing failures that traced back to one seemingly small design misstep: a pad that was too thin, a pivot placement that was off by a millimeter, or surface finishes that weren’t smooth enough for the oil film to form. Let’s dive into the core parameters that we (as a supplier) prioritize from the first consultation with a client to the final quality check before shipment.
First on the list: pad geometry, specifically pad length-to-width (L/W) ratio and pad thickness. This is where we start every design, because it directly impacts the load-carrying capacity and the stability of the oil wedge—the thin layer of lubricant that separates the rotating shaft from the stationary pad. Think of the oil wedge as a cushion: if the wedge is too thin or uneven, metal-to-metal contact happens, leading to friction, overheating, and wear. For years, the conventional wisdom was that a lower L/W ratio (around 0.5 to 0.7) worked best for high-speed, low-load applications, while a higher L/W ratio (0.8 to 1.2) was ideal for slow, high-load scenarios. But we’ve updated that advice with real-world testing from our in-house lab, where we’ve run 1,200-hour endurance tests on bearings for wind turbine gearboxes. Last year, a wind farm client came to us complaining of repeated pad wear on their new 2.5 MW turbines, where the original bearing had an L/W ratio of 0.6. Our team recalculated, adjusted the ratio to 0.85, and increased the pad thickness by 15% to accommodate the dynamic cyclic loads from the turbine’s rotor. The result? No failures in 18 months of operation, compared to the 9-month average they’d seen before. It’s important to note that pad thickness isn’t just about durability—too thin, and the pad will flex under load, disrupting the oil wedge; too thick, and you add unnecessary weight and cost that the application doesn’t need. We work with every client to tailor these dimensions, because a one-size-fits-all approach doesn’t exist for tilting pad thrust bearings.
Next, pivot design and placement. The pivot is the heart of the tilting function—every pad swings on its pivot, so the pivot’s type, location, and fit are non-negotiable. There are three primary pivot designs we specify: spherical pivots, knife-edge pivots, and flexure pivots, each with a specific use case. Spherical pivots are the workhorse for most industrial applications, because they offer large angular adjustment (up to 3 degrees) to compensate for significant shaft misalignment, which is common in heavy turbine and marine applications. Knife-edge pivots are lighter and simpler, so we use them for high-speed, low-load applications like small gas turbines, where minimal pivot friction is critical. Flexure pivots, a newer option, are ideal for ultra-precise applications like hydroelectric generators, where zero play is required to maintain consistent alignment at full load. But pivot placement is just as important as the pivot type. The optimal pivot location is along the “centroid of pressure” (COP) of the pad, which is roughly 55% of the pad’s length from the leading edge (the edge where the oil enters the pad’s surface). Get that placement wrong, and the pad will pivot unevenly, causing one edge of the pad to carry more load than the other, leading to premature wear. I remember a client in the mining industry who had a custom bearing made overseas where the pivot was placed 45% from the leading edge. Within 3 months, half the pads had chipped along the trailing edge from excess load. We repositioned the pivots to the correct 55% mark, and they’ve run without issues for two years. This isn’t just a design detail—it’s the difference between a bearing that lasts for years and one that needs replacement in months.
Lubrication system design parameters are the third critical piece of the puzzle, and this is where we often collaborate with clients’ engineering teams to get right. The two main lubrication methods for tilting pad thrust bearings are flood lubrication and jet lubrication, each suited to different operating conditions. Flood lubrication, where the entire bearing assembly is submerged in oil, is simple and effective for low-speed, high-load applications like heavy steel mill rolling stands. Jet lubrication, where oil is sprayed directly at the leading edge of each pad, is the go-to for high-speed applications like gas turbines, where centrifugal force would blow flood oil away. But it’s not just about how oil is delivered—it’s about oil flow rate, viscosity, and inlet temperature. Flow rate has to be calibrated to two needs: carrying away the heat generated by friction in the oil wedge, and maintaining a consistent oil film thickness. Too little flow, and the bearing overheats, leading to oil breakdown and metal contact; too much flow, and you waste energy on unnecessary oil pumping. Viscosity is another make-or-break factor: oil that’s too thin won’t form a stable wedge, while oil that’s too thick creates excess drag that reduces efficiency. For example, a 100 MW hydro generator we supplied bearings for last year required a 32 ISO viscosity oil at 40°C, with a flow rate of 120 liters per minute per pad. We tested every bearing with a custom lubrication rig to ensure that the oil film thickness was between 10 and 15 microns at full load—thin enough to minimize drag, thick enough to prevent wear. We also specify oil inlet temperature limits, typically between 40°C and 50°C, because oil viscosity drops sharply above 55°C, leading to failed lubrication.
Surface finish and material selection round out the core design parameters, and these are where we balance performance, cost, and longevity. The two main surfaces in contact are the rotating runner collar (attached to the shaft) and the stationary pad’s bearing surface. For runners, we almost always use hardened steel (typically 4140 or 4340 alloy steel) with a surface finish of 0.2 to 0.4 microns Ra. For pads, the material depends on the load and speed: babbitt (tin-based, with a small amount of copper and antimony) is the industry standard for most applications, because it’s soft enough to embed any small debris that gets into the bearing, preventing runner damage, while still being hard enough to carry the load. But for extreme high-load applications like marine diesel engines, we use aluminum alloy pads or even copper-lead alloy pads, which offer higher load capacity than babbitt. Surface finish for pads is equally critical: we aim for 0.1 to 0.3 microns Ra, because a rougher surface will create micro-cracks in the oil wedge, leading to friction. I’ve seen a client try to save money by having pads machined to 0.8 microns Ra, and within two weeks, the bearing had seized because the rough surface prevented the oil film from forming. It’s a lesson we always emphasize: surface finish isn’t a cosmetic detail—it’s a performance requirement.
Now, I know a lot of engineers reading this might be thinking, “These are all standard parameters—what makes your bearings different?” The truth is, while these parameters are non-negotiable, how we tailor them to each application is what sets our products apart. For example, when we design a bearing for a wind turbine, we account for variable loads that change with wind speed, so we add a small secondary pivot groove to let the pad adjust dynamically during low-load, high-speed gusts. For a marine bearing, we factor in the constant vibration from engine operation, so we specify a slightly thicker babbitt layer (0.5 mm instead of the standard 0.3 mm) to resist fatigue. Every application has unique quirks, and that’s why we don’t just offer off-the-shelf bearings—we work with clients to run finite element analysis (FEA) and computational fluid dynamics (CFD) simulations before manufacturing, to test how the bearing will perform under real operating conditions.

After 12 years in this industry, I’ve learned that tilting pad thrust bearings are often an afterthought in large machinery, but they’re the single most important component for supporting axial loads. A turbine, a generator, a cargo ship—all of it relies on that thin oil film between the pads and the runner to keep moving smoothly. That’s why getting the design parameters right isn’t just a technical exercise—it’s about keeping our clients’ operations running, avoiding costly downtime, and ensuring the safety of their equipment. If you’re an engineer or maintenance manager working with machinery that relies on tilting pad thrust bearings, I’d encourage you to ask questions about these parameters when you spec your next bearing. Don’t just look for a supplier that says they have “standard bearings”—look for a supplier that will work with you to tailor the design to your application’s specific loads, speed, and operating conditions. If you need to discuss a custom bearing project, or want to learn more about how we test and validate every component we ship, we’re here to help. Reach out to our team to start a conversation about your tilting pad thrust bearing needs, and let’s build a solution that keeps your equipment running reliably for years to come.
Thin Walled Babbitt Bearings References
Stansfield, F. (1970). Hydrostatic and Hydrodynamic Bearings. CRC Press.
Childs, D. (1993). Turbomachinery Rotordynamics: Phenomena, Modeling, and Analysis. John Wiley & Sons.
Neale, M. J. (Ed.). (1995). Tribology Handbook (2nd ed.). Butterworth-Heinemann.
Rowe, W. B. (1997). Hydrostatic Lubrication. Taylor & Francis.
Wenzhou Zhengbang Bearing Co., Ltd.
We are one of the most professional tilting pad thrust bearings manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy customized tilting pad thrust bearings at competitive price from our factory. If you have any enquiry about free sample, please feel free to email us.
Address: Units 1-1 and 3-1, Building 12, Yongxing Nanyuan Small and Micro Enterprise Startup Park, Binhai 2nd Road, Yongxing Subdistrict, Longwan District, Wenzhou City, Zhejiang Province.
E-mail: zbbearing@zbbearing.com
WebSite: https://www.zb-bearings.com/
